Future-Proof Cone Valve IBC Systems for High-Performance Powder Processing
Hygienic, modular, and efficient powder handling solutions for manufacturers across South East Asia — enabling fast recipe changeovers, dust-free operations, and segregation-free powder handling.
Our systems are trusted by manufacturers across South East Asia who require hygienic, flexible, and efficient powder handling — especially in multi-recipe, batch-based operations.
Designed for industries like pharmaceuticals, food & beverage, nutraceuticals, and chemicals, our solutions deliver safe, precise, and scalable powder processing with minimal cleaning time, no cross-contamination, and maximum productivity.
The Technology Behind Controlled Powder Handling
At the core of every Conebox IBC system is our Cone Valve technology — designed to provide controlled, contained and consistent discharge of powders and bulk solids.The cone valve is integrated into the bottom of the IBC and operates through a controlled vertical movement. As the cone lifts, it creates an opening that allows powder to discharge progressively from the container.
This controlled discharge principle is particularly valuable when handling powders that are cohesive, segregation-prone, fine, or otherwise difficult to flow.
How Does a Cone Valve Work?
1⏹️Closed
The cone remains seated at the base of the IBC, keeping the powder contained during storage and transport.
2🔼Opening
The cone lifts vertically to create an annular opening at the discharge outlet.
3⬇️Controlled Flow
The opening allows material to discharge progressively, with flow behaviour
dependent on powder characteristics and system configuration.4⏫Discharge
Material passes through the discharge interface into downstream equipment for further processing, transfer or packing.
Unlock the Key Advantages of Cone Valve IBC Technology
Our Cone Valve IBCs offer significant performance advantages over traditional butterfly valve or slide gate systems:
⚙️ Mass Flow Discharge
Prevent bridging, rat-holing, and inconsistent discharge — even with challenging or cohesive powders.
🛡️ No Segregation
Maintain blend integrity during transfer. Perfect for preserving uniformity in dry-mix and multi-ingredient formulations.
🛢️ Dust-Free, Hygienic Operation
Closed systems reduce dust emissions and product loss while meeting strict GMP and food-grade hygiene standards.
⏱️ Quick Recipe Changeovers
Batch-based IBC handling eliminates fixed lines, allowing for fast product switches without cross-contamination risk.
🚿 Reduced Cleaning Downtime
No need to clean downstream equipment between recipes — saving hours per changeover and increasing daily throughput.
🎚️ Controlled Powder Flow
Integrated Cone Valve technology allows precise flow control and accurate dosing — crucial for consistent batch processing.
📃 Multiple Recipes, Simultaneously
Use multiple IBCs in parallel to manage diverse products in the same facility — with complete batch traceability.
🏭 Modular & Scalable System
Start small and scale fast. Add more IBCs, filling/discharge stations, or automation features as your production grows.
🏷️ Future-Proof Solution
Our systems are designed for long-term use, supporting automation, traceability, and integration with Industry 4.0 platforms.
Whether you're handling free-flowing granules or sticky, cohesive powders, Cone Valve IBC systems deliver consistent, clean, and safe powder flow — every time.
From Cone Valve to Complete Powder Handling
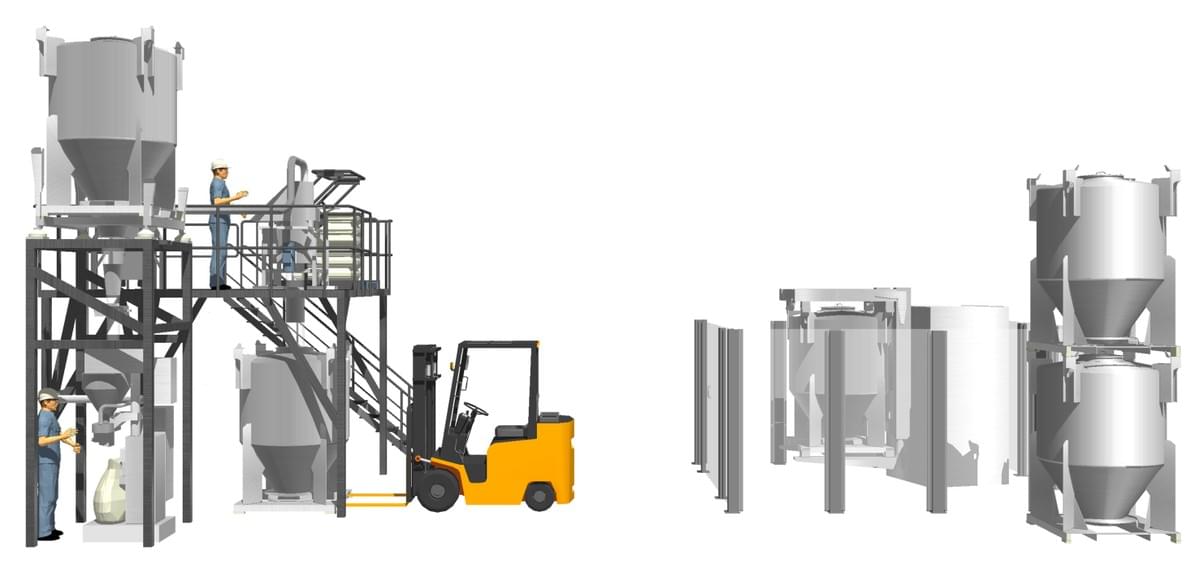
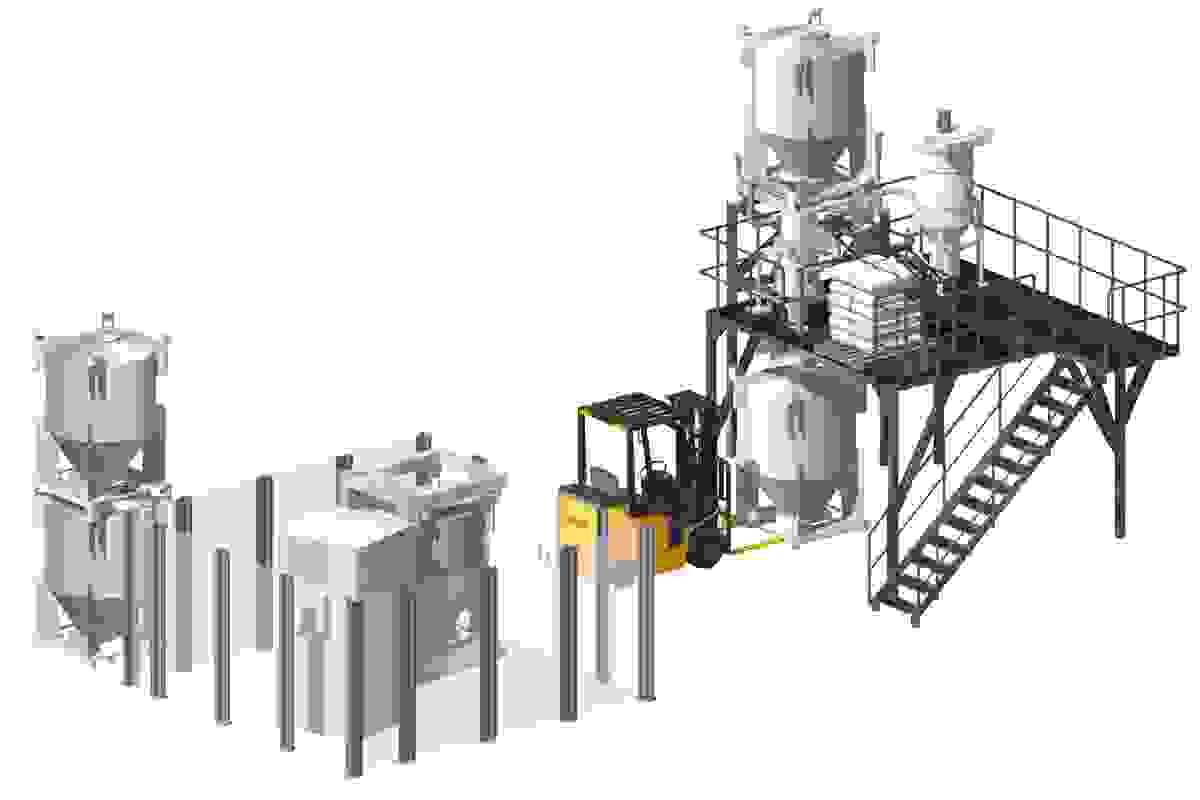
Cone Valve technology is not an isolated component. It can form the foundation of an integrated IBC powder handling process:
- 1
⬇️Filling
2⏹️Storage
3🔃Blending
4⚖️Weighing & Dosing
5⏫Discharge
6⤵️Transfer
7📦Packing
Conebox systems can be configured from a single IBC and discharge station to a fully automated powder handling solution incorporating filling, blending, weighing, cleaning and process automation.
Our Solutions
Explore our fully integrated powder handling systems based on Cone Valve IBCs:
- IBC Discharge Stations with Flow Control
- IBC Filling Stations
- Dosing & Weighing Integration
- IBC Blending with or without High Shear
- Cleaning Systems (WIP/CIP)
- Full range of IBCs (200L-3500L)
- Turnkey IBC Handling Systems
Need a single unit or a full turnkey system? We support your operations from concept to commissioning.
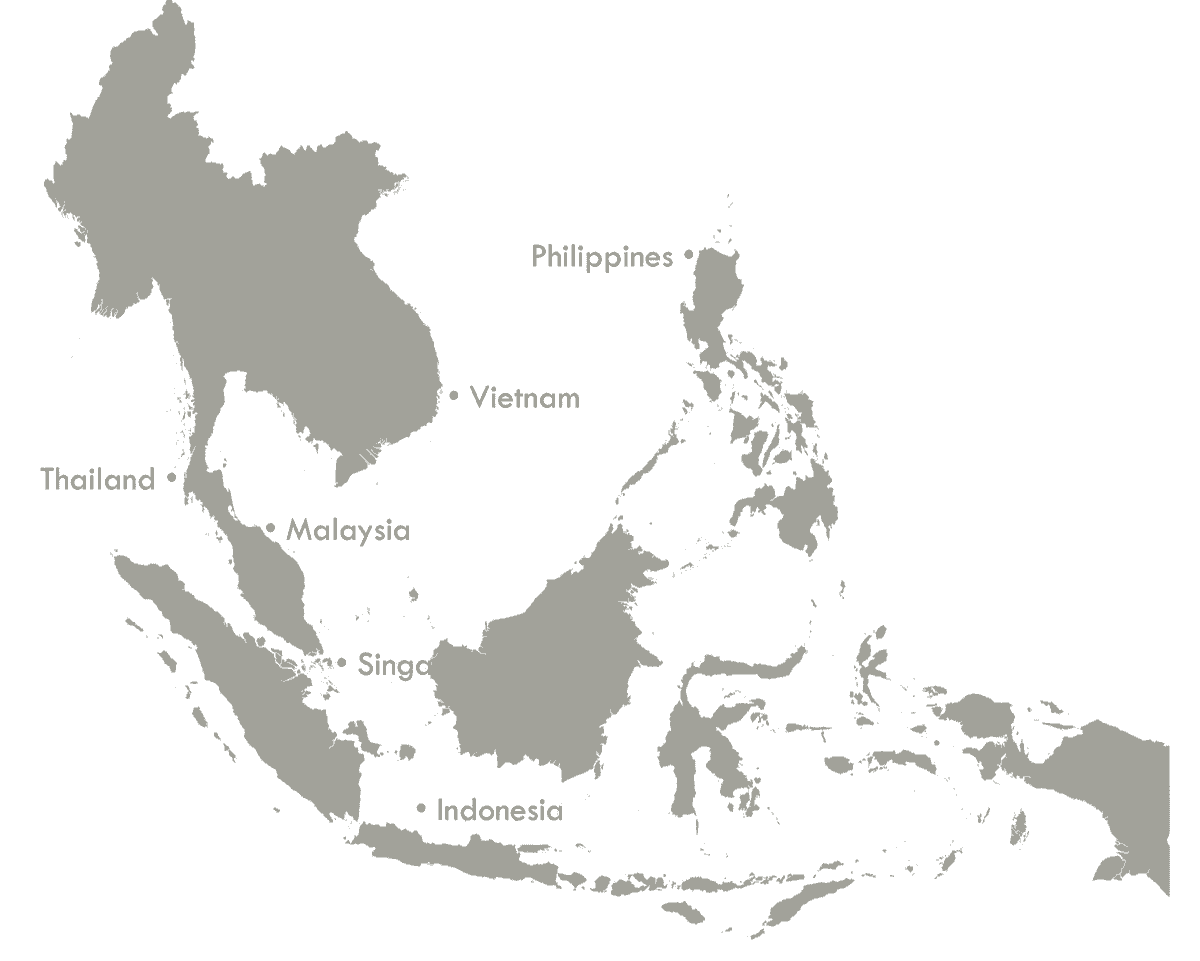
Designed for South East Asia’s Leading Industries
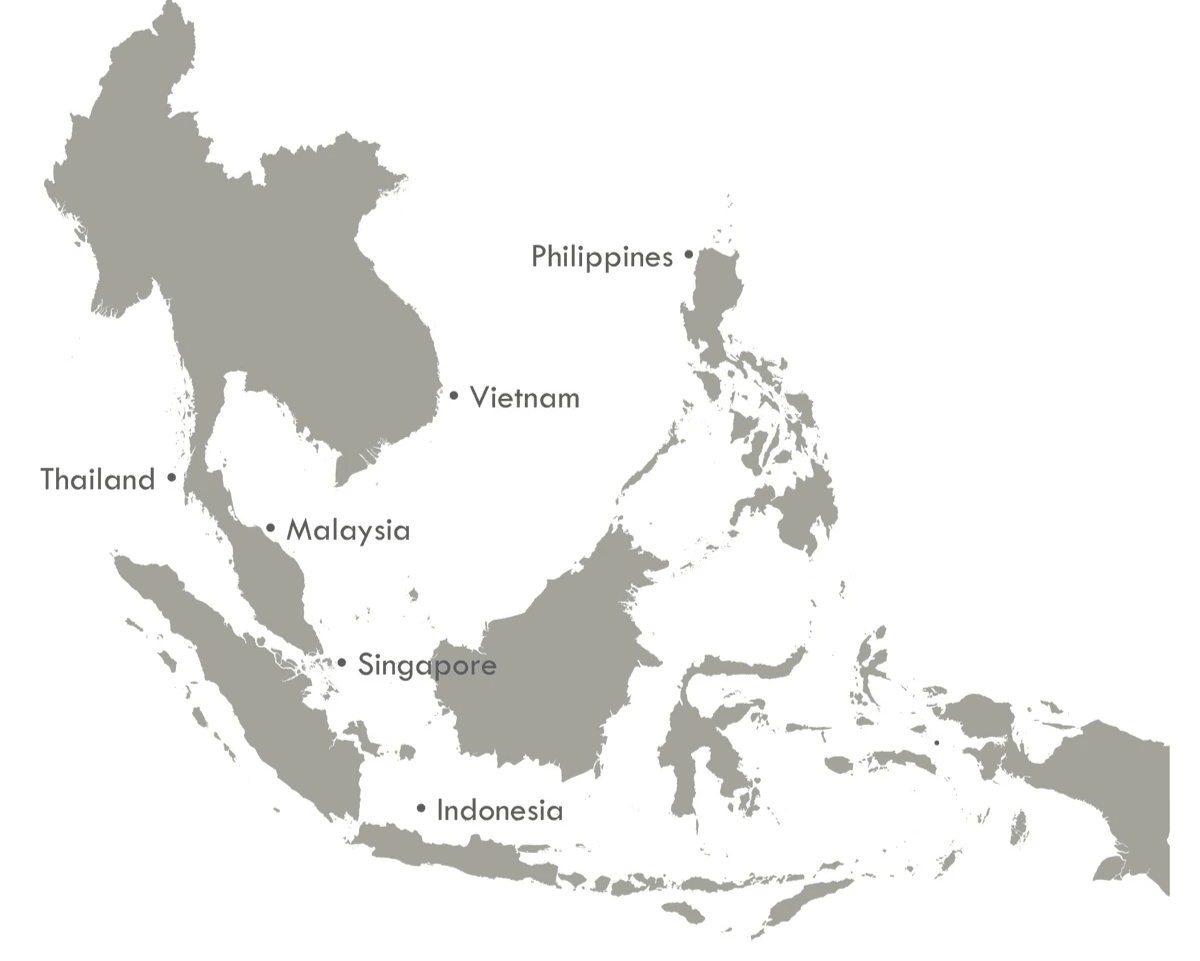
We proudly serve a growing customer base across ASEAN countries — offering full support in:
- Pharmaceuticals – API blending, granules, direct compression blends
- Food & Beverage – protein powders, milk derivatives, seasonings
- Nutraceuticals – vitamins, herbal powders, probiotics
- Chemical & Cosmetic Industries – pigments, resins, talc, base powders
Why Choose Conebox?
- Over 15 Years of Regional Experience
- Local Support in Southeast Asia
- Custom Solutions for Complex Powders
- Compliant with GMP, ATEX & FDA Standards
- Global Technology with ASEAN Expertise
Our Client Success Story
“Thanks to the Cone Valve IBC system, we now run three recipes side by side with zero cross-contamination and cut changeover time by 75%. It’s a game-changer for our multi-product facility.”
— Executive Director, Instant Beverages Manufacturer, Malaysia
Get in Touch
Speak with our IBC specialists today. Let’s build your next-generation powder handling system.
Ready to Upgrade?
Transform your powder handling with a hygienic, modular, and future-ready IBC system.
CONEBOX PTE. LTD. (202326932E)
160 Robinson Road, #14-04 Singapore Business Federation Center, Singapore 068914
Tel (SG): + 65 8678 3109 (Whatsapp)
Tel (MY): + 6010 246 2478
Website: www.conebox.co
Email: info@conebox.co
Copyright © 2023-Present.
Conebox Pte. Ltd. All Rights Reserved